Robots flawlessly repeat mistakes. That won’t happen with our solutions. Find out more about stable processes here!

Mounted points POLINOX PNER

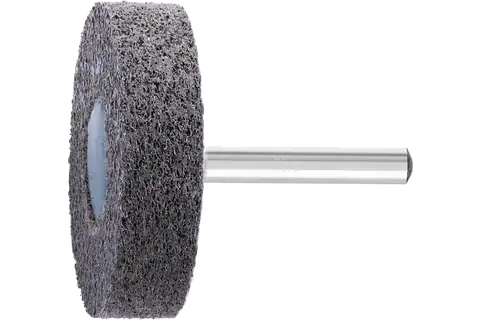
POLINOX pressed non-woven grinding point cylindrical shape PNER dia. 50x13 mm shank dia. 6 mm medium-hard SIC fine for finishing

PNER-MH ZY 5013/6 SIC F
Item number:
47700227
EAN:
4007220789841
New
Technical data Change variant

Login / Register
Choose options
Abrasive
Dia. external
Dia. shank
Grit size
Shape
Version
Width
Technical information
POLINOX pressed non-woven grinding point cylindrical shape PNER dia. 50x13 mm shank dia. 6 mm medium-hard SIC fine for finishing

Abrasive
Silicon carbide SiC/C
Dia. external
50 mm
Dia. shank
6 mm
Grit size
F (fine)
Length, shank
40
Max. RPM
10200 RPM
RPM, optimum
6400 RPM
Shape
ZY
Version
MH (medium-hard)
Width
13 mm
Packaging unit
5 pieces
Description

POLINOX grinding points PNER consist of multiple heavily compressed, non-woven layers, which are bonded together by a special grain/resin system. The different combinations of compression, fibres, grain and the appropriate bond result in non-woven products that offer a very good surface finish, high stock removal rate and long tool life. These tools can be used for a wide range of work on surfaces, from relatively coarse grinding to preparing the surface for polishing.

The version for straight grinders is particularly suitable for working on fillet welds and hard-to-reach contours or indentations.

Multiple heavily compressed, non-woven layers, which are bonded together by a special grain/resin system. The SiC version is ideally suited to demanding tasks on hard or sensitive materials.

The cylindrical shape ZY is ideal for grinding bores, radii and contours.

Special features
  • Particularly suitable for hard-to-reach indentations and contours.
  • High economic efficiency due to high abrasive performance and long tool life.
  • Produces very good surface quality.
  • Can be profiled as desired, enabling optimal adjustment to the contour.
Recommendations for use
  • For the best results, use at a recommended cutting speed of 10-20 m/s. This provides an ideal compromise between stock removal rate, surface quality, thermal load on the workpiece and tool wear.
  • Considerably reduce cutting speed for work on materials with poor heat-conducting properties, e.g. titanium and stainless steel.
Safety notes
  • For safety reasons, the maximum permitted rotational speed indicated must never be exceeded.
Materials that can be worked
Aluminium
Brass
Bronze
Cast steel
Cobalt-based alloys
Copper
Fibre-reinforced thermosetting plastics (GRP, CRP)
Hardened, heat-treated steels over 1.200 N/mm² (< 38 HRC)
Nickel-based alloys (e.g. Inconell and Hastelloy)
Stainless steel (INOX)
Steel materials with a hardness > 54 HRC
Steels up to 1,200 N/mm² (< 38 HRC)
Thermoplastics
Titanium
Titanium alloys
Zinc
Applications
Cleaning
Deburring
Roughening
Step-by-step fine grinding
Structuring (matt finishing, brush matting and satin finishing)
Surface work
Drive types
Flexible shaft drive
Straight grinder
Downloads

PFERD TOOLS Newsletter subscription

Register here free of charge for our PFERD TOOLS newsletter and receive all the latest news on products, services and promotions from the world of PFERD TOOLS on a regular basis.